 EN
What filter matching rule for dust proof cabinet cooling fan operating in cement factories
2026/09/30
Cement cabinets choke on dust. Learn the filter rule for an industrial cabinet cooling fan: G4/F7 media, IP rating, and pre-filter care.

2026/09/11
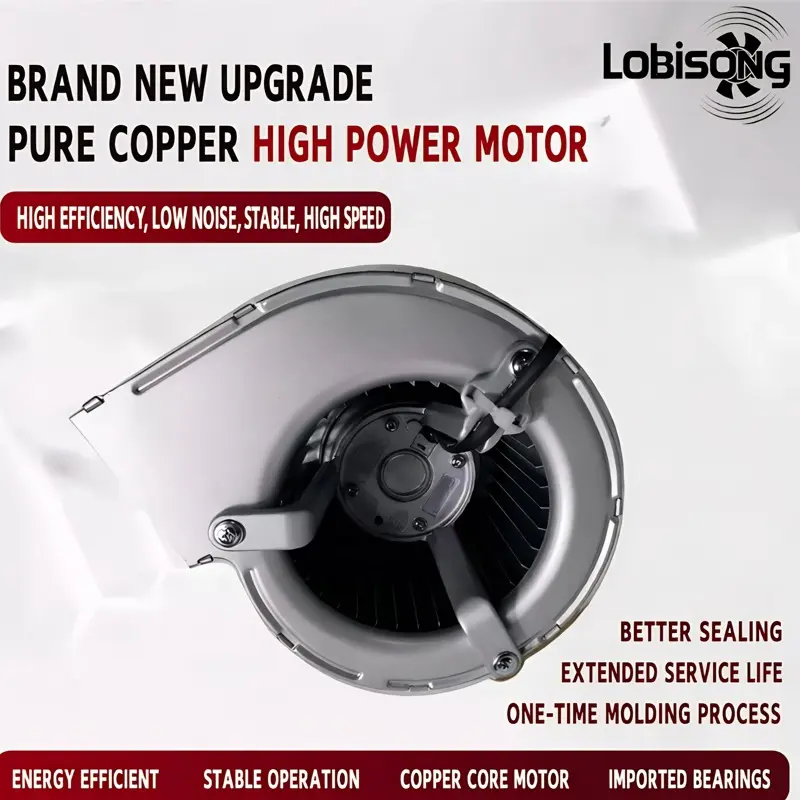
Mechanical processing releases more than chips and finished parts. Every day a CNC lathe floods its enclosure with coolant mist, a machining center sprays cutting oil, and a welding station throws metal fumes into the air. These aerosols settle as a sticky film on floors, rails and control cabinets. A centrifugal extractor fan industrial system captures that contaminated air at the source and keeps the workspace breathable.
Oil mist starts where metal meets a spinning tool. At high airflow velocity the coolant film on a cutting edge atomizes into fine droplets that ride the convection current away from the spindle. Welding arcs vaporize surface coatings and oils, then the vapor condenses into respirable oil mist as it cools. The droplet size spans sub-micron vapor to visible spray, so capture must handle both. Thermal lift near a hot tool keeps the aerosol buoyant, letting it travel before settling. A centrifugal extractor fan industrial pulls this stream toward the capture hood before it spreads across the shop.
Cutting oils and way lubes are viscous. When they hit a passive panel filter the grease bonds to the media and bridges the pores within hours. Filtration efficiency collapses, static pressure climbs, and the motor works harder for less air. Worse, the saturated pad becomes a fire load. As pressure drop rises, the fan draws less air per watt and the hood loses capture, so mist escapes into the room. Simple filtration alone cannot sustain a clean workshop ventilation loop in a heavy-oil environment.industrial centrifugal extractor fan, oil mist extraction, workshop ventilation, CNC coolant mist
Inside the unit a brushless outer-rotor motor spins an impeller at several thousand rpm. This is the heart of every centrifugal extractor fan industrial: as the mist-laden stream enters, centrifugal separation forces the heavier liquid phase outward. Droplets cannot follow the air's curved path, so they slam into the housing wall, coalesce, and drain into the collection chamber. The cleaned air continues to the exhaust duct. Pure copper windings and precision ball bearings keep the rotor stable under continuous duty. Blade geometry matters: backward-curved profiles resist fouling and keep the unit efficient as oil films build.industrial centrifugal extractor fan, oil mist extraction, workshop ventilation, CNC coolant mist
Filtration traps particles on a surface that fouls; centrifugal separation removes liquid by physics, not by clogging a media. For sticky oil mist the centrifugal extractor fan industrial approach holds performance long after a panel filter would be blocked. Many plants pair a centrifugal stage with a washable snap-on screen, gaining a second polish without the throwaway-media cost or the downtime of frequent change-outs. Centrifugal stages also tolerate the wide viscosity range found across shops, from thin grinding coolant to thick way oil, without a change in set-up.industrial centrifugal extractor fan, oil mist extraction, workshop ventilation, CNC coolant mist
On a centrifugal extractor fan industrial the collection chamber must slope to a drain so re-entrained oil cannot be sucked back into the airstream. The exhaust duct should keep a steady airflow velocity to avoid droplet dropout and pooling at bends. IP54 enclosure protection shields the drive and bearings from shop moisture, and a service port lets crews drain and wipe the chamber during planned maintenance.
Hot processes near extraction create real danger. NFPA 86 governs ovens and furnaces where combustible vapor accumulates, and it demands controls that limit ignition sources. A spark from a worn bearing or an exposed heater can ignite oil fog. Specifying thermally protected motors, anti-static belts, and properly grounded exhaust duct runs reduces that ignition path and keeps the installation inspectable. Where oil fog mixes with solvent vapors the blend can reach a flammable range, so ventilation and interlocks must be engineered, not guessed.
Regulators treat oil mist as a health hazard. OSHA permissible exposure limits for oil mist cap the concentration workers may breathe over a shift. ISO 45001 sets the framework for managing occupational health through controlled workshop ventilation and monitoring. Engineering the capture rate to those limits, then verifying with periodic air sampling, turns compliance from paperwork into a measurable safeguard. Record-keeping closes the loop: logged sample results show an auditor that the control works, not merely that equipment was bought.
A precision machining workshop ran flood-coolant mills with only passive filters. Floors turned slick, filters clogged weekly, and technicians reported headaches. The plant installed centrifugal capture units above each mill, ducted to a central collection tank. Within a month the floor film disappeared, filter change-outs dropped, and air samples cleared the exposure limit. Effect: fewer slip incidents, lower maintenance, and calmer inspections.
A well-selected centrifugal extractor fan industrial turns a fogged, hazardous cell into a controlled process. It removes oil at the source, protects workers, and cuts the fire load that sticky mist creates.
For procurement, inspect the motor type (pure copper windings, imported precision bearings), confirm IP54/IP44 rating, CE and UKCA documentation, and customizable voltage such as 115V/230V/400V. During use, drain the collection chamber on a schedule, check airflow velocity at the hood, and clean the washable screen. Match capacity to coolant type and duty hours rather than to catalogue peak figures.
What is the main difference between centrifugal and filter-only oil mist removal?
Answer: Centrifugal separation removes liquid by flinging droplets to a wall through rotation, so it does not depend on a media that clogs. Filter-only units trap oil on a porous pad that fouls quickly under sticky coolant. The first method holds performance in heavy-oil shops, while the second needs frequent pad swaps. Pairing both gives polish plus longevity without the throwaway-media cost.
Why does oil mist create a fire and explosion risk?
Answer: Oil fog forms a combustible aerosol near hot spindles, ovens, and welding arcs. A stray spark from a worn bearing or an exposed heater can ignite that vapor, and saturated filters add fuel load. Controlling ignition sources, grounding the exhaust duct, and limiting combustible vapor under NFPA 86 discipline reduces the chance of a flash fire in the extraction path.
How is an oil mist extractor mounted above a machining center?
Answer: A centrifugal extractor fan industrial mounts on a capture hood or enclosure roof above the mill, then connects to a sloped exhaust duct that drains to a collection chamber. Position the inlet where the mist lifts off the spindle, seal joints, and ground the run. Commission with an airflow check at the hood and a drain test before production resumes.
Where should the collected oil be drained and how often?
Answer: The collection chamber should drain to a sealed tank through a sloped bottom so re-entrained oil cannot return to the airstream. Drain frequency depends on coolant type and duty hours; a busy flood-coolant mill may need weekly service, while light-duty cells run longer. Inspect the chamber during planned maintenance and wipe residue to keep separation efficiency steady.
Can existing workshop ventilation meet OSHA oil mist limits without extraction?
Answer: Often not. Passive general ventilation dilutes but rarely captures mist at the source, so local concentrations near spindles stay high. Engineering capture with a centrifugal stage pulls contaminated air before it spreads, making OSHA permissible exposure limits achievable. Pair source extraction with periodic air sampling to confirm the workshop stays within the regulated concentration over a full shift.

2026/09/30
Cement cabinets choke on dust. Learn the filter rule for an industrial cabinet cooling fan: G4/F7 media, IP rating, and pre-filter care.

2026/10/07
Right wall-mount height for an industrial axial exhaust fan: room volume, free clearance, brackets, and recirculation control.

2026/10/08
An ec motor fan links to BMS via Modbus, 0-10V and PWM for demand-based cooling, energy scheduling and automatic sensor-driven speed control.

2026/10/06
A radial exhaust fan removes grease, fumes, and odors from food-processing workshops with capture velocity and hygienic washdown design.

2026/10/05
Learn antistatic treatment for industrial cabinet cooling fan in electronics workshops—ESD-safe housing, ionizable plastics, and cleanroom compatibility.

2026/10/04
Discover how a brushless dc servo delivers precise wind speed control for laboratory cooling fans with closed-loop PID feedback and laminar airflow.
